CASE STUDY
Back to ProjectsNEW PRODUCT LAUNCH · 2024
Lollipop Packaging Commercialisation
Wipro Consumer Care
RolePackaging Executive, R&D
OrganizationWipro Consumer Care & Lighting
TimelineAug 2024 – May 2025
NPDBarrier FilmsHigh-Speed WrappingCommercialisationAutoCAD KLD
Packaging FormatsPrimary + Secondary
CommercialisationConcept to Scale-Up
Specifications100+ Specs Released
Overview
Bringing a new confectionery product to market requires precision control over moisture sensitivity, machine-runnability on high-speed lines, child-friendly opening ergonomics, and vibrant retail shelf appeal.
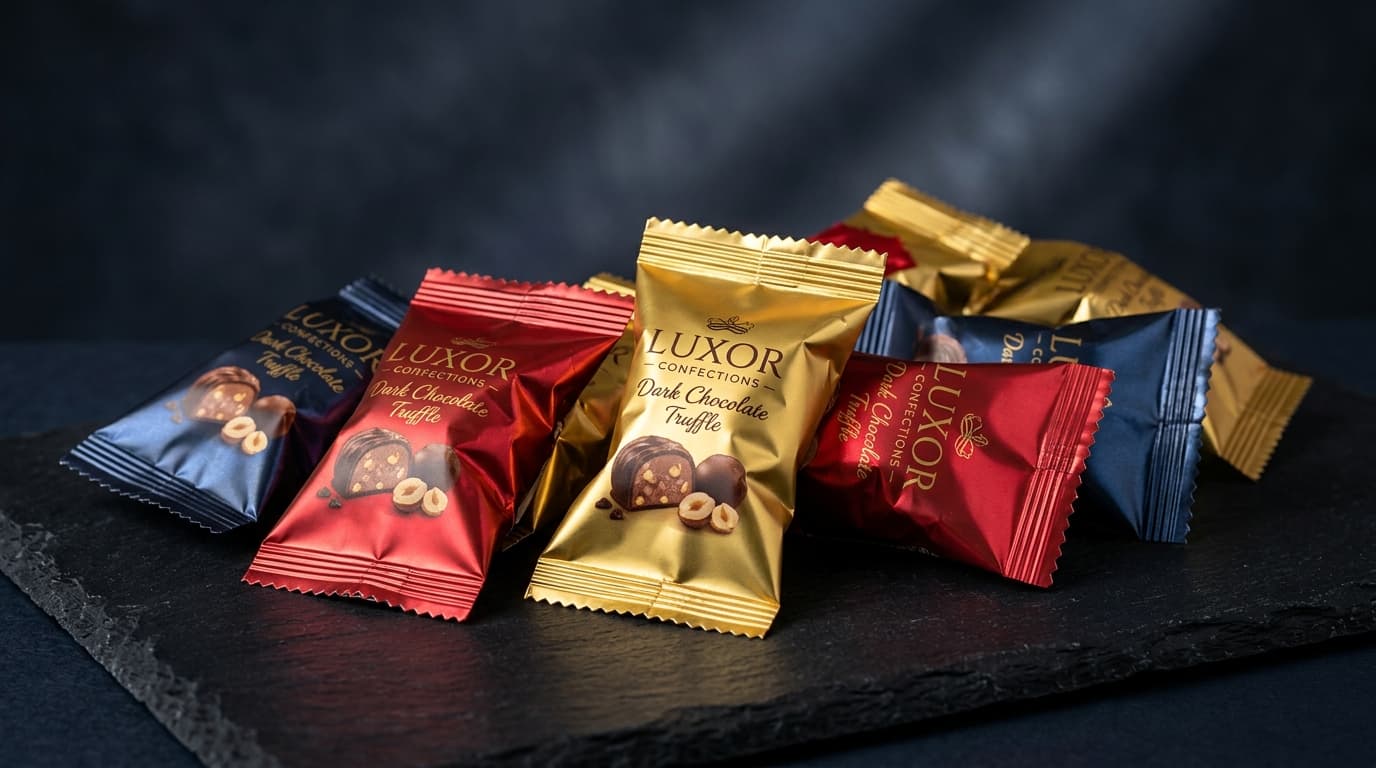
This project encompassed the end-to-end development of the primary barrier twist-wrap and secondary pouch/carton packaging for a new confectionery launch within Wipro Consumer Care.
Technical Considerations & Barrier Requirements
- Hygroscopic Sensitivity: High sugar-confectionery absorbs ambient moisture rapidly in tropical humid climates, leading to stickiness, graining, and color degradation if water vapor transmission rates (WVTR) are inadequate.
- High-Speed Machine Runnability: High packaging line speeds (over 300 units/min) demand consistent coefficient of friction (COF), static dissipation, and thermal dead-fold retention.
- Food Safety Compliance: All raw materials, printing inks, and adhesives had to strictly adhere to Food Contact Materials standards under FSSAI regulations.
Development Milestones
1. Substrate Specification & Barrier Engineering
- Evaluated high-barrier metallized cast polypropylene (CPP) vs. bi-axially oriented polypropylene (BOPP) laminates to balance optimal moisture barrier (WVTR < 1.0 g/m²/day) with cost efficiency.
- Verified seal integrity and cold-seal adhesive release profiles to prevent flavor contamination.
2. AutoCAD Key Line Drawings (KLD) & Tooling
- Drafted precise 2D KLDs for wrapper cut-off lengths, eye-mark positioning for optical photo-sensors, and secondary hanging-hole pouches.
- Built comprehensive Bills of Materials (BOM) and technical packaging specifications approved across factory production sites.
3. Factory Line Trials & Transit Validation
- Executed pilot and full-scale factory line trials, tuning seal jaw temperatures, wrapper tensioners, and twist-head grippers.
- Validated real-time ambient and accelerated shelf-life stability tests (38°C / 90% RH) over a 6-month evaluation period.
Commercial Outcome
- On-Time Nationwide Launch: Commercialised on schedule with zero line downtime during commercial commissioning.
- Extended Shelf-Life: Maintained product crispness and flavor profile across peak monsoon conditions without moisture ingress.
- Robust Documentation: Handed over standardized, audit-ready Packaging Material Specifications (PMS) to QA and plant operations teams.
Previous ProjectYardley Lotion Dispensing OptimizationNext ProjectTransit Safety & Vibration Testing Standardisation
Next Steps
Let's ConnectCurious about sustainable packaging?
Let's connect to discuss sustainable materials, regulatory audits, or end-to-end commercialisation.